
Designing 3D-printed gears: module, tooth count, profile shift and backlash
How to choose module, tooth count and ratio for 3D-printed gears, why small pinions need profile shift, how much backlash to leave and print settings for clean teeth.
Published
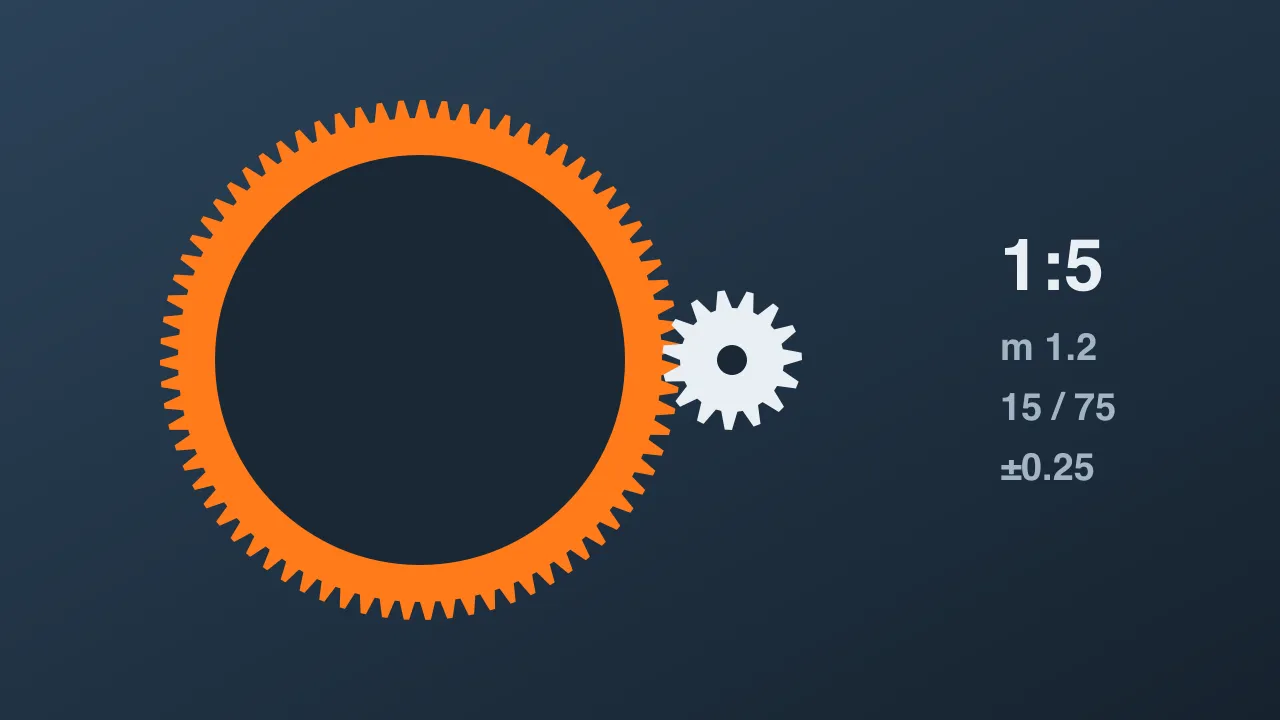
3D-printed gears are good enough for most small machines: turntables, presses, winches, spoolers. They run smoother than you might expect if a few numbers are right. This post uses the gear pair from the 360° turntable as the example: a 15-tooth pinion, a 75-tooth ring gear, module 1.2.
Module: the size of the teeth
Module (m) sets how big the teeth are. Two gears only mesh if they have the same module.
- Pitch diameter: d = m × z (z is the tooth count). Example: 15 teeth × 1.2 = 18 mm; 75 teeth × 1.2 = 90 mm.
- Center distance: a = m × (z1 + z2) / 2 = 1.2 × 90 / 2 = 54 mm.
With a 0.4 mm nozzle, module 1 or more prints crisp teeth. Module 0.5–0.8 is printable but the teeth are thin, wear faster and need very fine layers. Module 1.2–1.5 is the safe zone for moderate loads.
Gear ratio
Ratio = driven teeth / driving teeth. 75 / 15 = 1:5: the platter turns 5 times slower than the motor with about 5 times the torque. The 28BYJ-48 tops out around 12 rpm, so the platter turns at about 2.3 rpm, nicely slow for product shots.
Small gears need profile shift
With the standard 20° pressure angle, gears with fewer than 17 teeth suffer undercut: the tooth root gets carved away, weakening the tooth and spoiling the mesh. The fix is profile shift:
- Shift the pinion positive, for example +0.25: thicker tooth roots, no undercut.
- Shift the big gear by the opposite amount, −0.25: the shifts sum to zero, so the center distance stays 54 mm.
Most gear tools (build123d gear libraries, Fusion, OpenSCAD) have a profile shift parameter; just fill it in.
Backlash
Printed gears need clearance between teeth because printed dimensions are off by a few tenths of a millimeter and plastic expands when warm. Without it, gears bind or squeal.
- About 0.1–0.2 mm suits a 0.4 mm nozzle. The turntable uses about 0.14 mm.
- Easy method: increase the center distance by 0.1–0.15 mm, or use your gear tool’s backlash parameter.
- Test-print the gear pair on its own (the pinion prints very quickly) before committing to the big ring gear.
Mounting on the motor shaft
- The 28BYJ-48 shaft is Ø5 with two flats down to 3 mm. A printed D-shaped hole of about 5.1 / 3.1 mm is a snug push fit, no screw needed.
- Round shafts without flats: use an M3 set screw into a nut trapped in the gear hub, or a brass insert.
Print settings
- Print flat, gear face on the bed. The teeth are loaded along the layers, which is the strongest direction.
- 0.12–0.16 mm layers for a smooth tooth profile.
- 4–5 perimeters or 100% infill: teeth nearly solid.
- PLA is fine for light loads; PETG is tougher, chips less and handles heat better.
- A dab of grease or PTFE lubricant on the teeth makes them run noticeably quieter and last longer.